Office Address: Sunmoon Science Park, 985 Xingzhong Road, High-Tech Zone, Bengbu, China Factory Address: Mohekou Industrial Park, Huaishang District, Bengbu, Anhui, China Contact: Amina Zhang Phone: 0086-18055211309 FAX: 0086-552-3822922 Mobile: +86 18055211309 WebSite: www.iotachem.com
www.siliconeoil.net
Email: info@siliconeoil.net QQ:
|
Hydride Polydimethyl siloxane IOTA 616
Low viscosity vinyl silicone oil IOTA 218
Vinyl-terminated T-structured polydimethylsiloxane IOTA-22713
Single-ended vinyl silicone oil IOTA 22711
Polyether-modified polysiloxane IOTA-2204
Polyether Silicone Oil IOTA 2H57
Polyether Silicone Oil IOTA-23667
IOTA 6289 Methyl Silicone Resin for Concrete and Stone
Polyethylsiloxane Fluids IOTA 2056 PES
Ethyl Silicone Rubber IOTA 2056 HTV
Ethyl Silicone Rubber IOTA 2056 GUM
Single-terminated trimethoxyl-terminated silicone oil IOTA-2307
Mercapto modified silicone oil IOTA-280
IOTA 5532 Methoxytriphenylsilane
IOTA 5722 methoxy(methyl)diphenylsilane
Tetramethyldisilazane IOTA 5205H
Super Hydrophobic Nano Ceramic Coating IOTA ST6
Fluoro Silicone Gum
Self-drying Silicone Resin IOTA 6605L
Self-drying Silicone Resin IOTA 6604
Methyl silicone resin IOTA 6080
IOTA 6608/6609 Pure Organic Silicone Resin Emulsion
IOTA 6607 Epoxy Organic Silicone Resin Emulsion
IOTA 6606 Acrylic Organic Silicone Resin Emulsion
IOTA 1501 Cyclopentasiloxane and Dimethiconol
IOTA 201-1 Octamethyltrisiloxane
Carbinol Silicone Oil IOTA 28300
Phenol Terminated Silicone Oils
1,3-Bis(3-aminopropyl)-1,1,3,3-tetramethyldisiloxane IOTA2458

Hexamethylcyclotrisilazane IOTA-N202
Water-based silicone resin IOTA 6850S
Water-based silicone resin IOTA 6830S
Polyester modified silicone resin IOTA 6072A
Polyester modified silicone resin IOTA 6072-50D
Polyester modified silicone resin IOTA 6072-15
Polyester modified silicone resin IOTA 6038A
Methyl phenyl silicone resin IOTA 6156C
Methyl phenyl silicone resin IOTA 6153D
Methyl phenyl silicone resin IOTA 6056D
Methyl phenyl silicone resin IOTA 6056
Methyl phenyl silicone resin IOTA 6053G
Epoxy-modified silicone resin IOTA E60
Epoxy-modified silicone resin IOTA E30
Epoxy-modified silicone resin IOTA E25
Epoxy-modified silicone resin IOTA 6063-55
Alkyd modified silicone resin IOTA 6057
Acrylic polysiloxane resin IOTA BXS-90
Acrylic modified silicone resin IOTA 6146A
Acrylic modified silicone resin IOTA 6146
Acrylic modified silicone resin IOTA 6046
Organic Polysilazane IOTA 9283
Organic Polysilazane IOTA 9150K
IOTA 9028 Dichloro-bis(chloromethyl)silane
Non-foaming defoaming wetting agent IOTA 4100
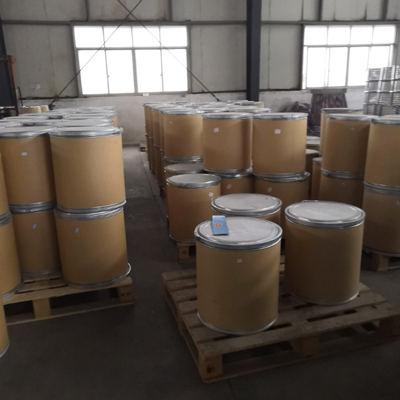
Eco-friendly Solid Silicone Resin IOTA 6106
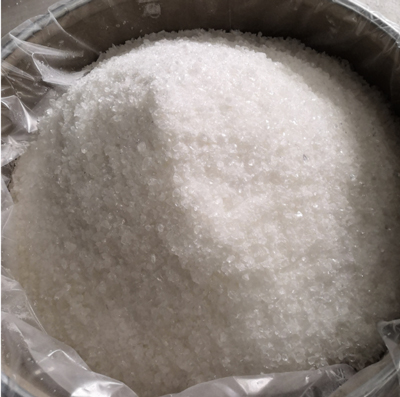
Eco-friendly Solid Silicone Resin IOTA 6105
Eco-friendly Solid Silicone Resin IOTA 6103
IOTA 3090A acrylic modified silicone resin
IOTA 1153D methyl phenyl silicone resin
IOTA 1146 acrylic modified silicone resin
IOTA 1127 polyester modified silicone resin
IOTA 1123 silicone resin intermediates
IOTA 1072A polyester modified silicone resin
IOTA 1063-55 epoxy modified silicone resin
Transparent super hydrophobic nano coating IOTA ST5
Carboxyl Silicone Oil IOTA 2520
Double-ended hydroxypropyl silicone oil IOTA 2030
Double-ended alcohol hydroxyl long-chain alkyl silicone oil IOTA 2865H
Double-ended alcohol hydroxy silicone oil IOTA 2110
Diol hydroxyl single-end long-chain alkyl silicone oil IOTA 2866
Diol hydroxyl single-end silicone oil IOTA 2176
Hydroxyl terminated methyl vinyl silicone oil IOTA 1203V
Acrylic Silicone Oil IOTA 2205
Single-ended hydroxypropyl silicone oil IOTA2050
Alcohol hydroxy single-ended long-chain alkyl silicone oil IOTA 2861
Single-ended alcohol hydroxyl silicone oil IOTA 2170
Side Chain Acrylate Modified Silicone Oil IOTA 170
Acrylic Silicone Oil IOTA 2220
Polycarbosilane adhesive IOTA H11500
Polycarbosilane adhesive IOTA H21500
Borosilazane adhesive IOTA H21400
Silazane Adhesive IOTA H21000
Silazane adhesive IOTA H31000
High temperature curing silicone sealant IOTA H1400
Modified cyanate ester adhesive IOTA RH3400C
Silicone resin modified cyanate ester Adhesive IOTA R3400
Fast curing high temperature resistant putty IOTA R31800F
High temperature resistant putty IOTA R31800
Silicone sealant IOTA R1400
Phenolic Modified Cyanate Adhesive IOTA R3600
Fasting curing silazane adhesive IOTA R3800F
Silazane ceramic precursor adhesive IOTA R31000
Silicone oxynitride adhesive IOTA R3800
High temperature resistant silicone adhesive IOTA R2400
Hexamethylcyclotrisiloxane IOTA D3
high temperature resistant water-based nano ceramics coating IOTA ST4
Highest hardness Nano-coating in room temperature cured IOTA ST3
Waterborne nano high hardness self-cleaning coating IOTA ST2
Waterborne nano high hardness self-cleaning coating IOTA ST1
Low volatile silicone oil
Low viscosity hydroxyl fluoro silicone oil IOTA40F
Modified hydroxypropyl silicone oil (aqueous system)IOTA2040
Single-ended hydroxypropyl silicone oil IOTA2050
Bicomponent structured adhesive
IOTA 7000 (6000 Anti-fogging agent)
Epoxy double heads IOTA-010
Acrylate modified silicone oil IOTA 2032
Acrylate modified silicone oil IOTA 2031
IOTA 201-2 Dimethicone 2cst
Epoxy silicone oil chain extender IOTA 105-1000
Epoxy polyether silicone oil
IOTA 345 Cyclopentasiloxane and Cyclohexasiloxane
Drift control adjuvant IOTA-331
IOTA 9970 Organopolysilazane for car coating
Silicon dioxides for coating
Hydrophobic series silica
IOTA FINE-SIL520A Silicon Dioxide
IOTA FINE Silicon dioxide
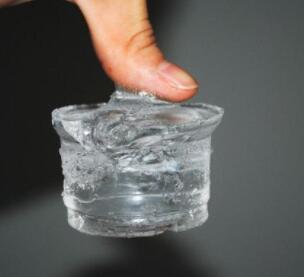
IOTA 96212 Silicone Elastomer Gel
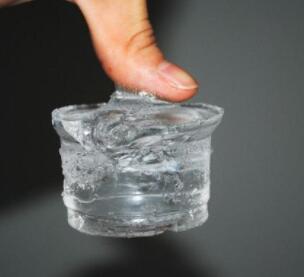
IOTA 96211 Silicone Elastomer Gel
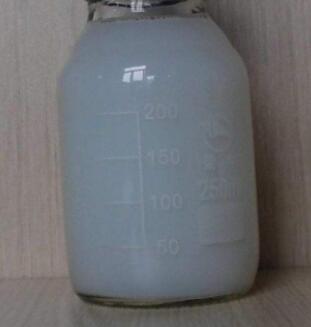
IOTA 96082 Silicone Resin Elastomer Suspension
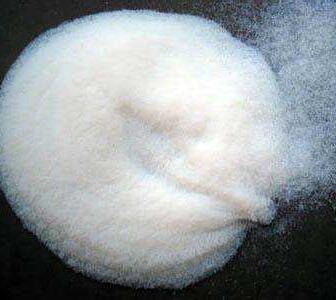
IOTA 96061 Silicone Elastomer Powder
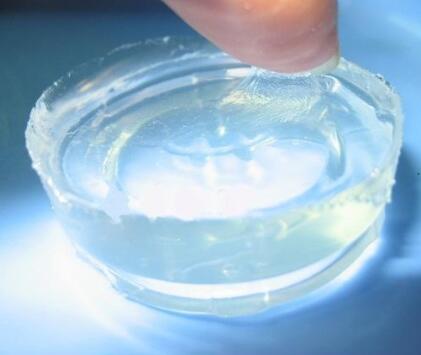
IOTA 96004 Silicone Resin Elastomer Gel
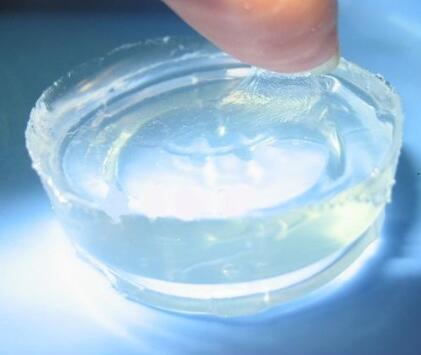
IOTA 9609 Silicone Elastomer Gel
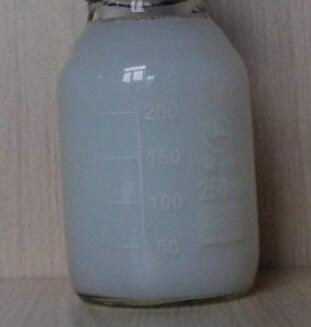
IOTA 9608 Silicone Elastomer Suspension
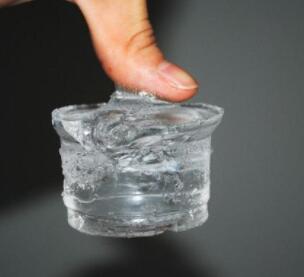
IOTA 9607 Silicone Elastomer Gel
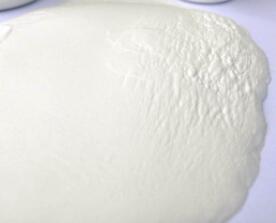
IOTA 9606 Silicone Elastomer Powder
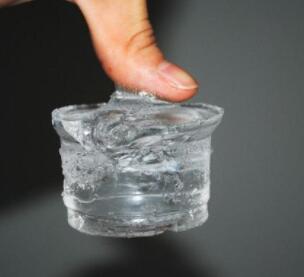
IOTA 9600D Silicone Elastomer Gel
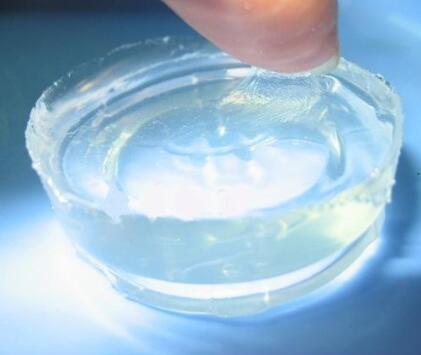
IOTA 9600B Silicone Elastomer Gel
IOTA 9600 Silicone Elastomer Gel
Organic polyborosilazane (Potteryable precursor polymer) IOTA 9120
Nano silica dispersion IOTA 100F1, IOTA 100F2
Hydrophobic Silica IOTA 90-02
Hydrophobic Nanometer Silica IOTA 90-01
Hydrophilic type nano-silica IOTA 100
Anti-graffiti silicone resin IOTA-TC1
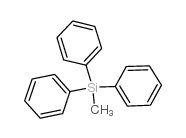
IOTA 5803 Methyltriphenylsilane
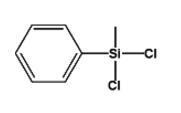
Methyl phenyl dichlorosilane IOTA5804
Organic polysilazane IOTA 9108
Organic polysilazane IOTA 9118
High transparency mold making silicone rubber
Food grade silicone rubber for mold making
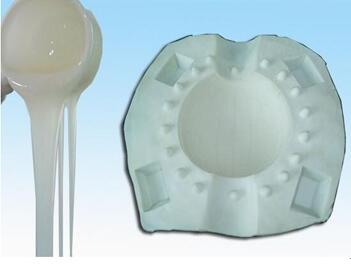
Condensation type mold silicone rubber
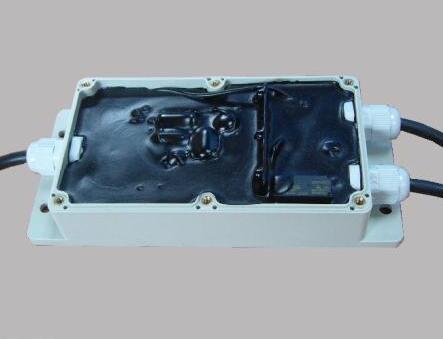
High refraction index phenyl silicone packing gel IOTA 34255
IOTA 255-54 DIPHENYL DIMETHICONE
High temperature resistant silicone oil IOTA-255A
Organic silicon industrial cleaning agent IOTA2018
Sealed silicone grease IOTA 2014
Thermal Grease IOTA 2013
Lubricating silicone grease IOTA2012
OctaMethyltetrasiloxane IOTA2101
Methyl-bis(trimethylsilyloxy)silicon IOTA2100
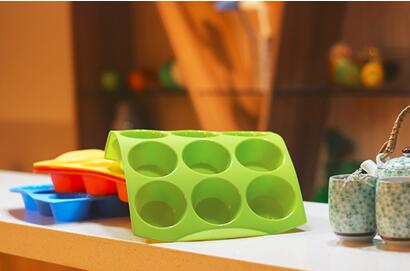
Silicone products multi holes cake mold IOTA 41007
silicone rubber material for Flame retardant high temperature resistant IOTA 26E9-40,50,60
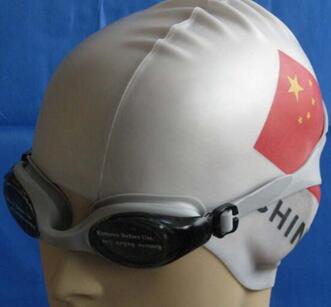
Silicone rubber material for swimming class equipment with IOTA351-20, 30, 40, 856-20, 221-20
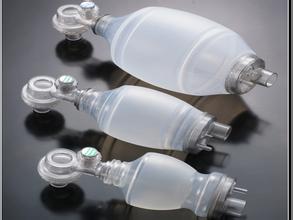
Silicone rubber material for Medical apparatus and instruments IOTA5971-60*, 70* ,80*,IOTA971-60* ,60K
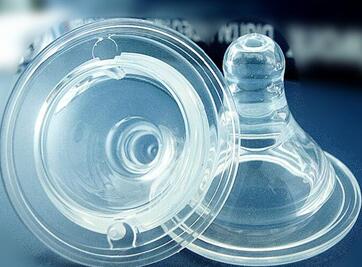
Liquid silicone rubber material IOTA-6120 15, 20, 20-H
Silicone rubber material for auto parts IOTA 231-20*
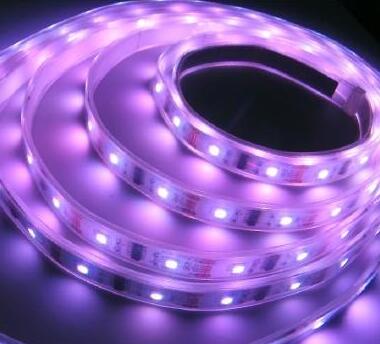
Silicone rubber material for wire, tubular product IOTA4366-30, 40, 50, 60, 70, 80
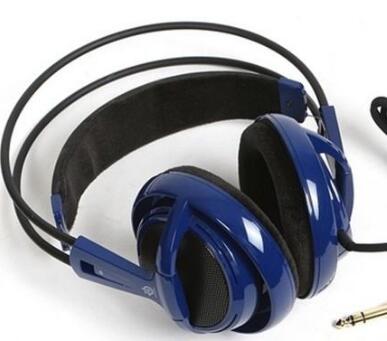
Silicone rubber material for wearable digital electrical accessories IOTA 151-30A, 40A, 50A, 60A, 70A, 80A
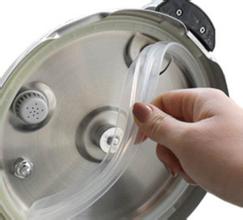
Silicone rubber material for home appliance accessories and miscellaneous pieces IOTA151-10, 20, 30, 40, 50, 60, 70, 80, 90
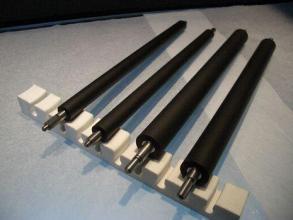
Silicone rubber material for industrial products IOTA9241-20*,30*,40*,50*,60*
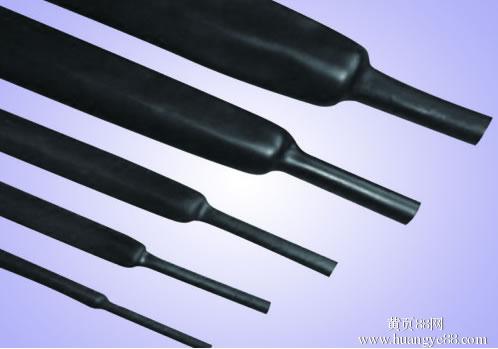
Silicone rubber material for electrical power, communication IOTA141-40*, 50*, 60*
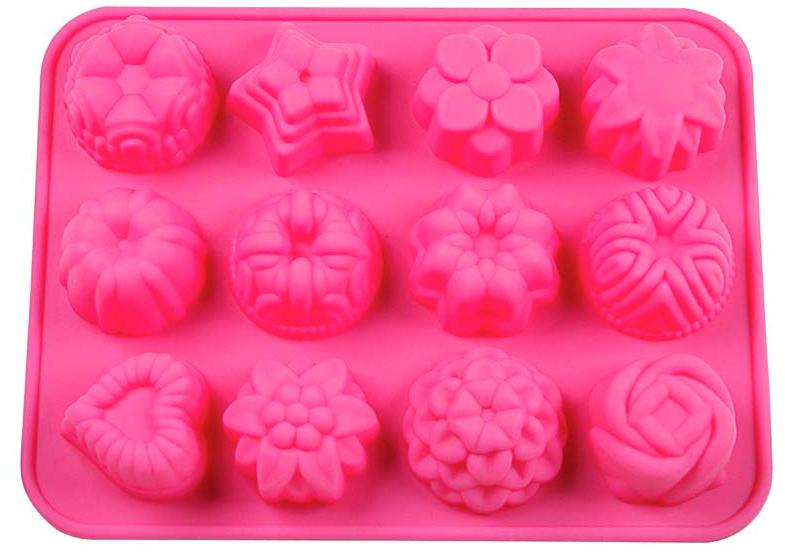
Silicone rubber material for Kitchen utensils and appliances industry class IOTA151-10, 20, 30, 40, 50, 60, 70, 80, 90
Silicone rubber material for office automation IOTA151-30, 40, 50
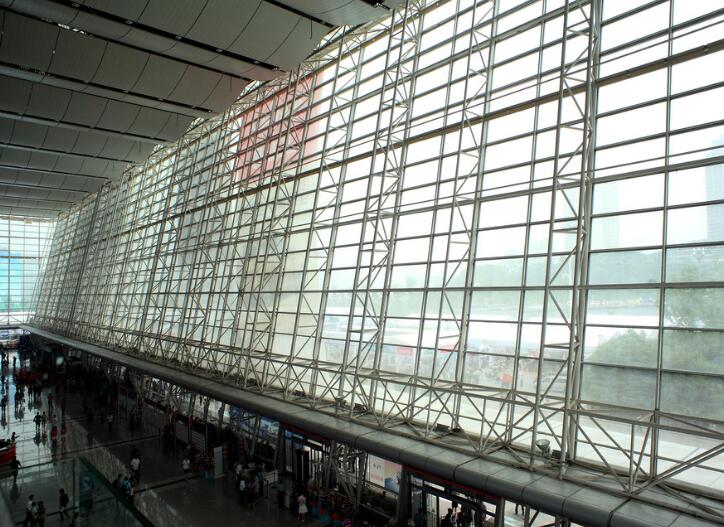
IOTA GF998 Fire Resistant Silicone Weatherproofing Sealant
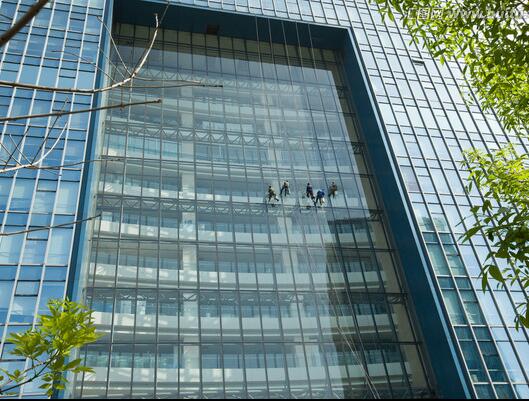
IOTA 1098 High Performance Silicone Weatherproofing Sealant
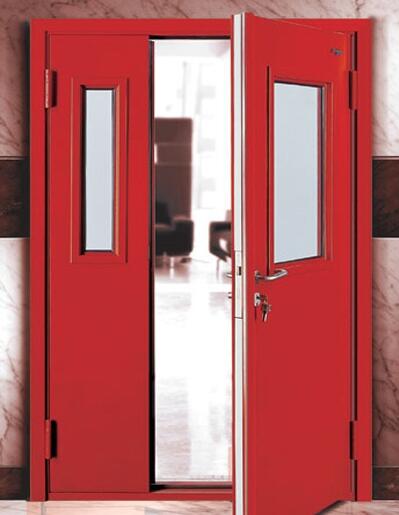
IOTA GF999 Fire Resistant Silicone Structural Glazing Sealant
IOTA 1092 High Performance Silicone Structural Glazing Sealant
IOTA 998 Silicone Weatherproofing Sealant
IOTA 997 Silicone Sealant For Stone Applications
IOTA 995 Silicone Sealant For Total Vision System
IOTA 992 Silicone Structural Glazing Sealant
IOTA DJ310 Hollow glass hot melt butyl rubber
IOTA 119 Fire Resistance Silicone Sealant
IOTA 997 Silicone Sealant For Stone Applications
IOTA 993 Silicone Sealant for Skylight
IOTA 887 Dry hanging stone elastic rubber
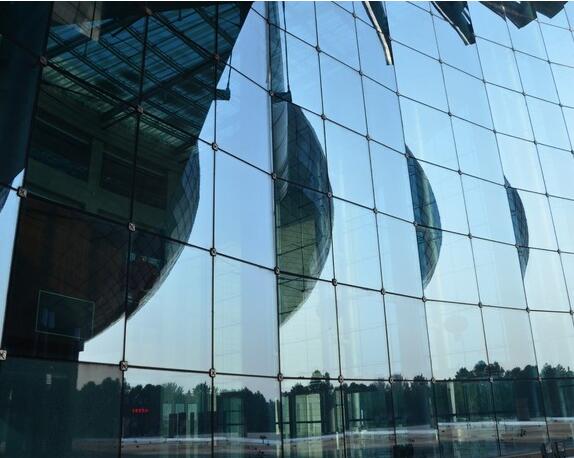
IOTA 886 Silicone Structural Insulating Glass Sealant
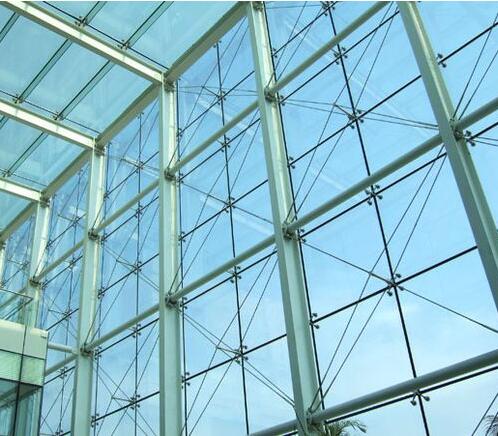
IOTA 882 Silicone Insulating Glass Sealant
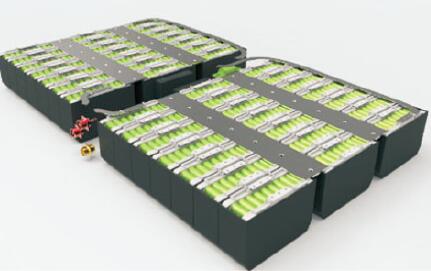
IOTA GZ series Thermal conductive silicone
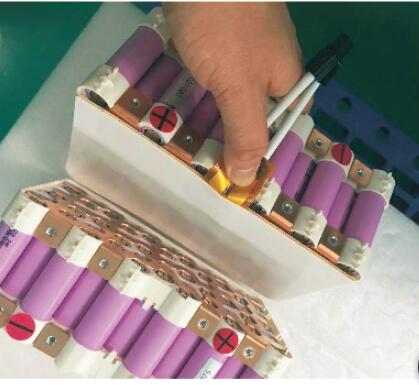
IOTA 3400 Silicone heat conductive gasket
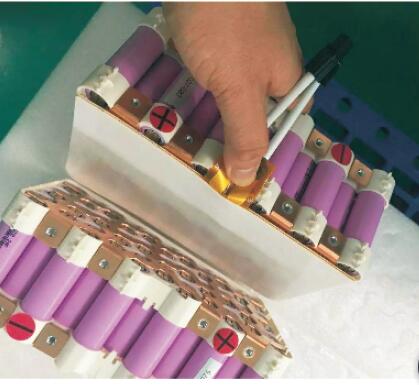
IOTA 3300 Silicone heat conductive gasket
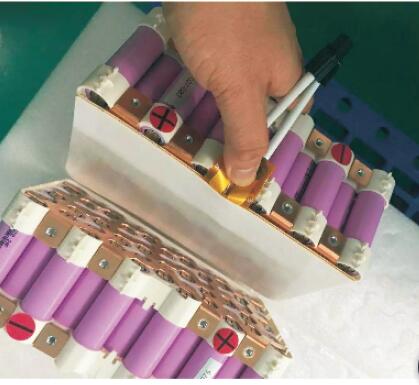
IOTA 3100 Silicone heat conductive gasket
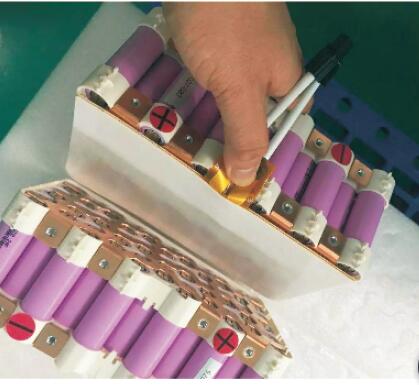
IOTA800FG Thermal insulator sheet
Cationic hydroxy silicone oil emulsion IOTA-2051
Anionic hydroxy silicone oil emulsion IOTA-2052
Epoxy silicone oil emulsion IOTA-1051
Hydrogen silicone emulsion IOTA 2021
Precipitated Silica IOTA9002
Silicone wax
IOTA SA408FG Thermally conductive double-sided adhesive tape
IOTA 4815W single component silicone sealant
IOTA 4815Z single component silicone sealant
IOTA 4815C One component silicone sealant
IOTA DJ330 Hot melt butyl
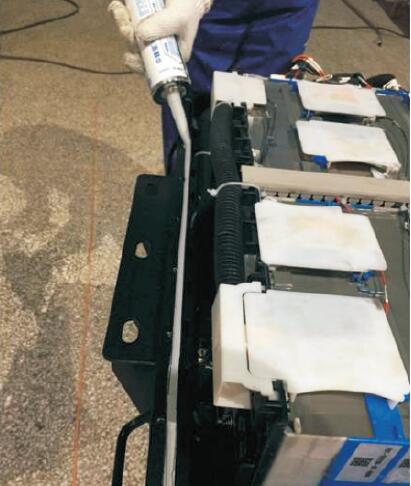
IOTA 4926 Silicone sealant for new energy automotive safety power
IOTA 4808 Silicone Electronic Potting Sealant
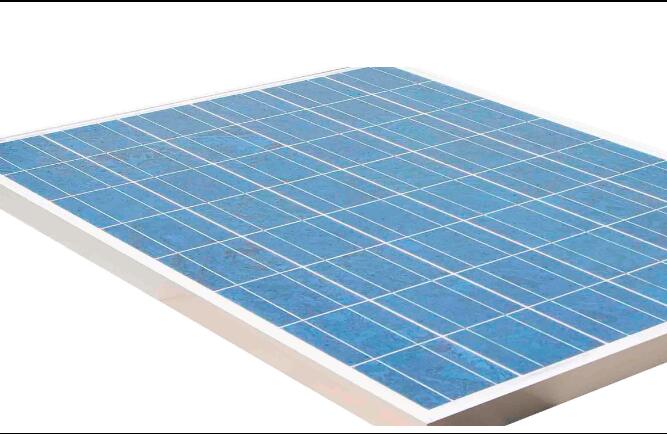
IOTA 888A Silicone Sealant for Solar Modules
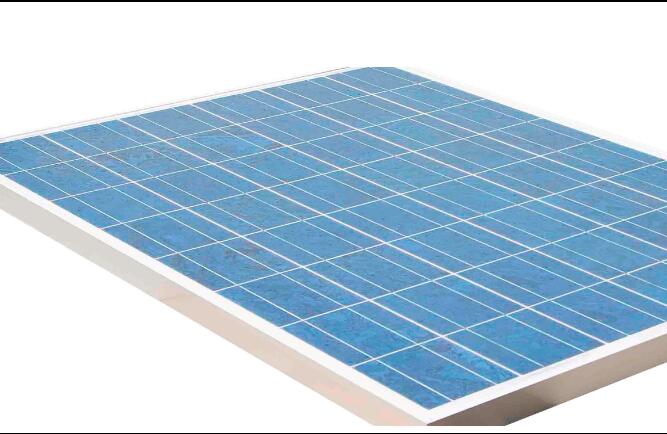
IOTA 855 Silicone Sealant for Solar Modules
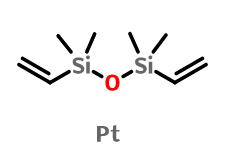
Platinum(0)-1,3-divinyl-1,1,3,3-tetramethyldisiloxane (the platinum catalyst) IOTA-8100
High temperature resistant silicone emulsion IOTA 240
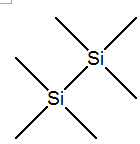
Hexamethyldisilane IOTA-5002
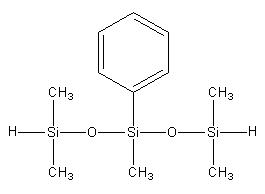
Pentamethylphenyl dihydrotrisiloxane IOTA-2238
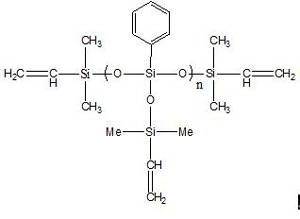
Vinyl terminated T-type phenylpolysiloxane IOTA-253
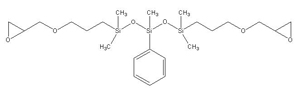
Epoxy-terminated phenyltrisiloxane IOTA-279
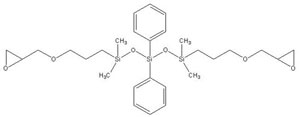
Epoxy-terminated phenyltrisiloxane IOTA-278
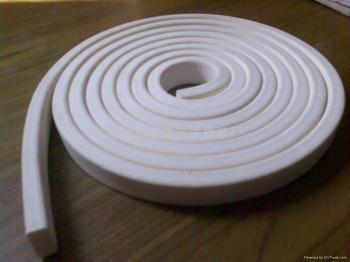
High elastic foam silicone strip IOTA-4801
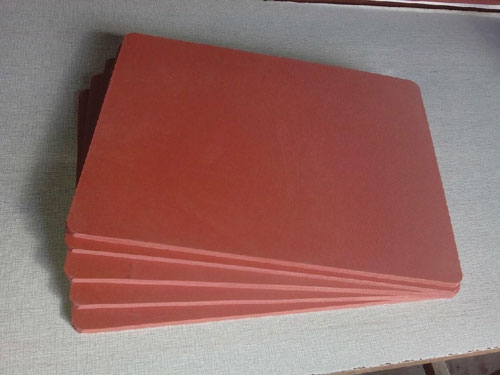
High elastic silicone foam sheet IOTA-4800
Phenyl silicone oil emulsion IOTA PEMUL 255
New type of silicone chain extension agent IOTA-4001
High refractive index plasticizer IOTA-9006
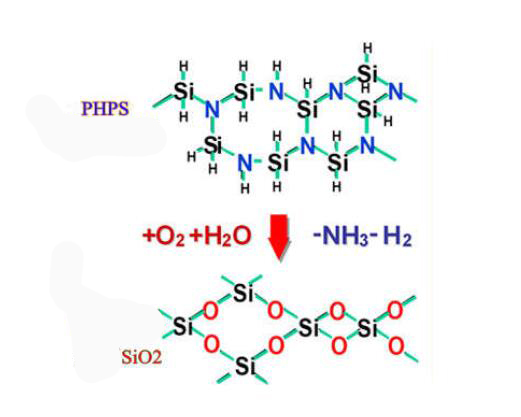
Perhydropolysilazane IOTA-PHPS
Heat Curable Coating Resin IOTA-OPSZ-1800
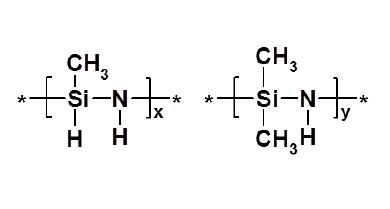
Organopolysilazane IOTA-OPSZ-9150
LED GEL refractive index regulator IOTA-9005
High refractive index silicone oil IOTA-259A
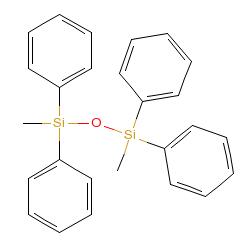
Dimethyltetraphenylsiloxane IOTA 259
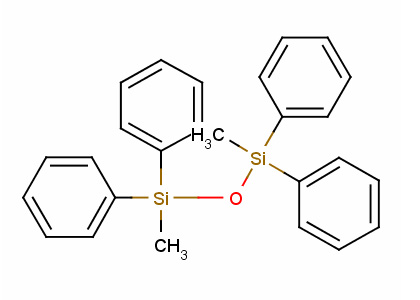
Tetraphenyldimethyldisiloxane
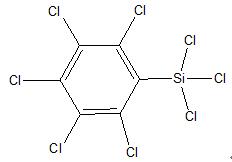
Pentachlorophenyl trichlorosilane
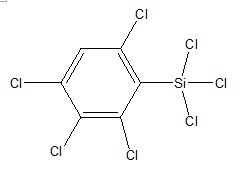
Tetrachlorophenyl trichlorosilane
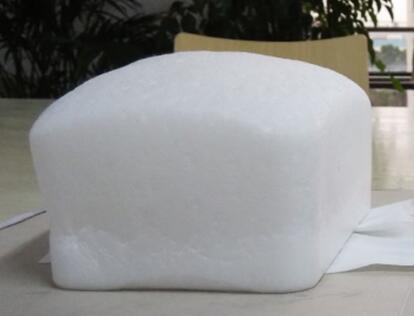
AB Liquid Silicone rubber foam IOTA-663
IOTA 201-1.5 Dimethicone 1.5cst
Silicone waterproof coating IOTA-301
Copolymer resin series mold materials for foam lost casting IOTA-STMMA
Long Glass Fiber Reinforced Polyamide IOTA-LFT-PA
Long Glass Fiber Reinforced Polypropylene IOTA-LFT-PP
Methylphenyl silicone resin IOTA-B202
Phenyl silicone resin IOTA-B201
Epoxy-modified silicone resin IOTA H-60
Epoxy-modified silicone resin IOTA-H-30
Polyester modified silicon resin IOTA-1062G
Modified silicone resin IOTA-1057
Pure silicone resin IOTA-1056D
Pure silicone resin IOTA-1056
Pure silicone resin IOTA-1053G
Polyester modified silicone resin IOTA-1046
Polyester modified silicone resin IOTA-1038A
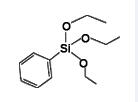
Phenyltriethoxysilane IOTA-531
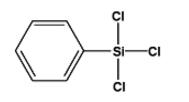
Phenyltrichlorosilane IOTA-525
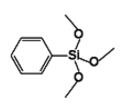
Phenyltrimethoxysilane IOTA-530
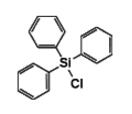
Triphenylchlorosilane IOTA-529
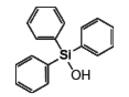
Triphenylsilanol IOTA-528
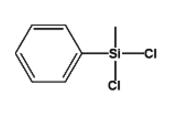
Methylphenyldichlorosilane IOTA-527
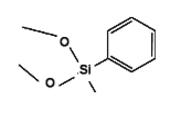
Methylphenyldimethoxysilane IOTA-526
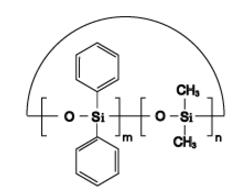
Dimethyl Diphenyl Cyclics IOTA-524
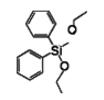
Diphenyldiethoxysilane IOTA-523
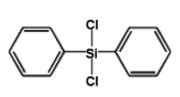
Diphenyldichlorosilane IOTA-522
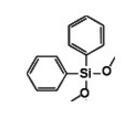
Diphenyldimethoxysilane IOTA-521
Silicones for Technical Fabrics and Leathers IOTA-TCS-7001
PHENYL SILICONEGUM(HTV)IOTA- 34
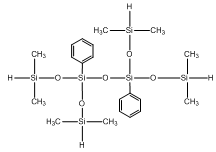
Diphenyl tetrasiloxane IOTA 234
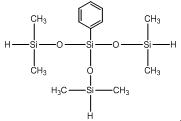
Phenyl-tris(dimethylsiloxy)silane IOTA 235
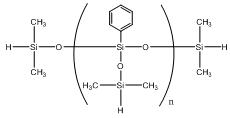
Phenylsilsesquioxanes hydrogen-terminated IOTA 233
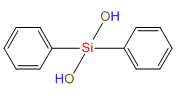
Dihydroxydiphenylsilane(DPSD) IOTA R05
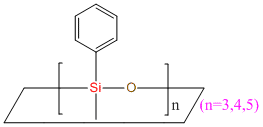
Cyclophenylmethicone IOTA R21
High security hydroxyl silicone oil for fumed silica IOTA 1203D
Linear hydroxyl silicone oil IOTA 1203M
Hydroxyl blocking methyl vinyl silicone oil IOTA 1203V
Methoxy blocking polymethyl silicone oil IOTA 1204A
Ethoxy blocking polymethyl silicone oil IOTA 1204B
Methyl phenyl methoxy silicone oil IOTA 1204C
DIMETHICONE IOTA DM 10
DIMETHICONE IOTA DM50 - DM1000
DIMETHICONE IOTA DM5000 – DM60000
Cyclopentasiloxane IOTA CM5 A2
Low Viscosity Silicone Oils IOTA PDMS 47V3 - 47V10
Middle Viscosity Silicone Oils IOTA PDMS 47V50 - 47V1000
High Viscosity Silicone Oils IOTA PDMS 47V5000 - 47V500000
Personal care silicone oil IOTA 29161
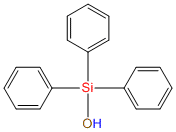
Triphenylsilanol IOTA R06
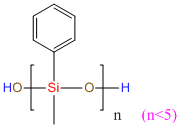
MePhOH-group silicone oil IOTA R32
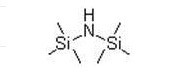
Hexamethyldisilazane(HMDS) IOTA 011
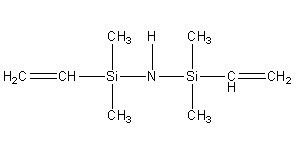
Vinyl silazane IOTA 51001
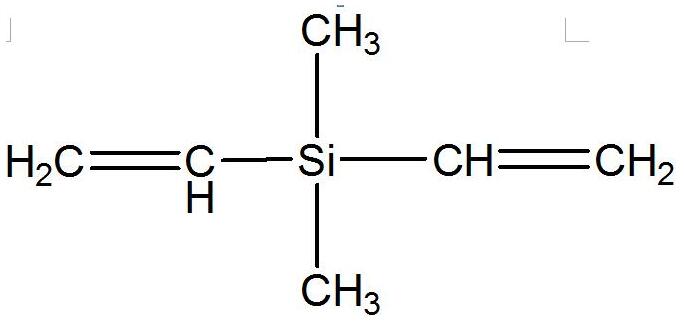
Dimethyldivinylsilane IOTA-501
Dual-head vinyl silicone oil IOTA VM-19
Multi-vinyl silicone oil IOTA VM-26
Cyclopentasiloxane dimethiconol IOTA 1021 IOTA 1022
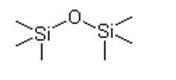
Hexamethyldisiloxane IOTA 005
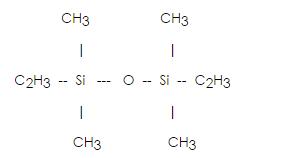
Divinyltetramethyldisiloxane(Vinyl double heads) IOTA 1002
Methylphenyldiethoxysilane IOTA-826
Diethoxydiphenylsilane IOTA-814
Diphenyldimethoxysilane IOTA-813
Phenyltriethoxysilane IOTA-802
Phenyltrimethoxysilane IOTA-801
Trimethoxysilylpropanethiol IOTA-590
3-Mercaptopropyltriethoxysilane IOTA-580
3-Ureidopropyltriethoxysilane IOTA-1160
γ-Ureidopropyltrimethoxysilane IOTA-1524
Anilino methyl triethoxysilane IOTA-42
Bis(trimethoxysilylpropyl)amine IOTA-1170
3-(2-Aminoethylamino)propyl-diethoxymethylsilane IOTA-5702
N-(2-aminoethyl)-3-aminopropylmethyl-dimethoxysilane IOTA-602
N (2-aminoethyl) -3-aminopropyltriethoxy-silane IOTA-910
N (2-aminoethyl)-3-aminopropyltrimethoxy-silane IOTA-792
3-(Diethoxymethylsilyl)propyl methacrylate IOTA-671
3-(Triethoxysilyl)propyl methacrylate IOTA-670
3-Methacryloxypropylmethyldimethoxy silane IOTA-571
3-methacryloxypropyltrimethoxysilane IOTA-570
3-Glycidoxypropyltrimethoxysilane IOTA-560
Vinyl tris(2-methoxyethoxy) silane IOTA-172
Dimethicone and Dimethiconol IOTA1403
Cyclopentasiloxane (and) Cyclotetrasiloxane (and) Dimethiconol IOTA1401
Methyl phenyl vinyl silicone rubber IOTA 120
Hexamethyldisilazane(HMDS) IOTA 011
Dimethyl Vinyl Ethoxy Silane (Vinyl single end ) IOTA-DVES
Trimethylchlorosilane M3
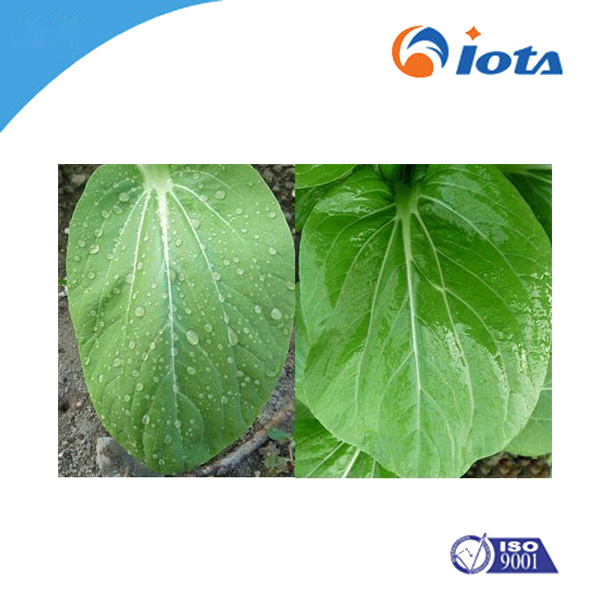
Powder Agricultural Silicone synergist IOTA2001
High temperature resistant release agent emulsion IOTA-257-60
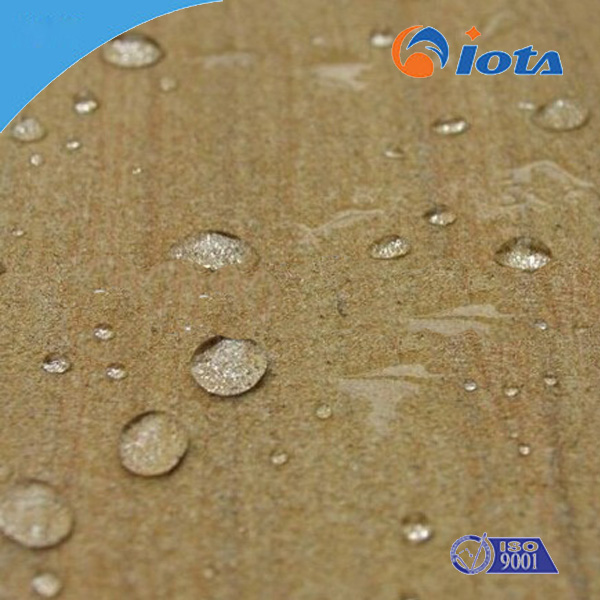
IOTA BP9500 Building protective waterproofing agent
Silicones for Technical Fabrics and Leathers IOTA 7001
IOTA 1647V75 Organo Functional
Leather processing waterproofing agent IOTA 1669
IOTA 70827A EMULSION CATALYST
Water Repellent IOTA EMUL 269
Water Repellent Treatment IOTA WR 68
Building Protection Water repellent additive IOTA BP 9705
Water based coating release agent IOTA MR5900
Solventless methyl silicone resin release agent IOTA RES 9515
Release agent IOTA 2206
Universal defoamer agent IOTA C585
High-performance silicone-based organic silicon compound IOTA C583
High-performance silicone-based organic silicon compound IOTA C581
Black liquor defoamer IOTA C563
Silicone defoamers IOTA C545
Low refractive LED Encapsulants
Methyl vinyl MQ silicone resin IOTA-AM
Methyl hydrogen cross-linking agent IOTA-AF
Octaphenyl cyclotetrasiloxane IOTA-AKT
Smooth and standing silicone oil for cotton IOTA 805
Super soft hydrophilic block silicone oil for cotton IOTA J50A
Super soft smooth hydrophilic block silicone oil for cotton IOTA N30
Smooth and soft silicone oil for cotton IOTA 817
vinyl ketone group, the crosslinking agent IOTA-91
Phenyltris methylethylketoximio silane IOTA-36
Methyltris(methylethylketoxime)silaneblend IOTA-32
Methyltrimethylethylketoximesilaneblend IOTA-31
Tetraethxoysilane-40 IOTA-130(Si40)
Ethyl silicate / Four oxygen radical IOTA-130(Si28)
Tetramethoxysilane (methyl orthosilicate) IOTA-5101
Methyltriethoxysilane IOTA-150
1,2-bis trimethoxysilyl ethane IOTA-26
Poly methyl triethoxysilane IOTA-23
Methylethyl triacetoxy silane IOTA-18
Methylpropyltriacetoxysilane IOTA-17
Propyl triacetoxy Silane IOTA-16
Ethyl triacetoxy silane IOTA-15
Modified methyltriacetoxysilane IOTA-13
Modified Methyltriacetoxysilane IOTA-12
Di-t-butoxydiacetoxysilane IOTA-11
Methyltriacetoxysilane IOTA-10
Mercaptopropyltriethoxysilane IOTA580
Vinyltris methoxyethoxysilane IOTA 172
Vinyltriethoxvsilane IOTA 151
aminopropylmethyldiethoxysilane IOTA 902
aminopropylmethyldimethoxysilane
Aminopropyltriethoxysilane IOTA 550
Trimethoxysilane IOTA 160
Construction sealant Oxime
Construction sealant Acetic
High transparent liquid silicone rubber LSR IOTA 6300
High tear strength and high temperature vulcanized silicone rubber IOTA HD
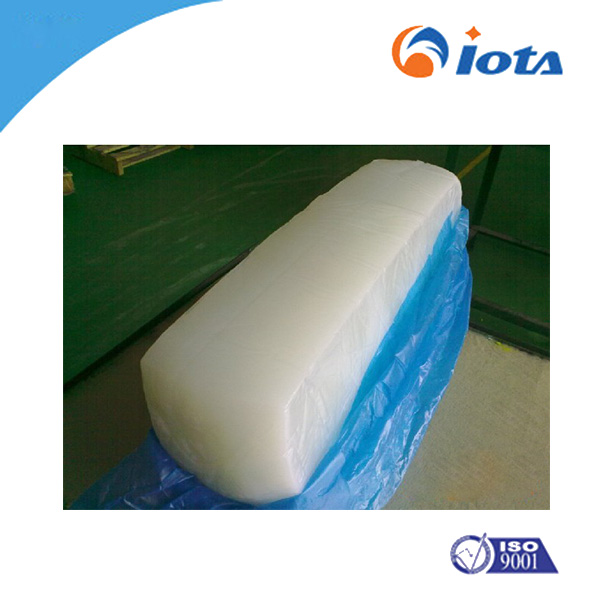
Safety cable silicone rubber MF IOTA 8465
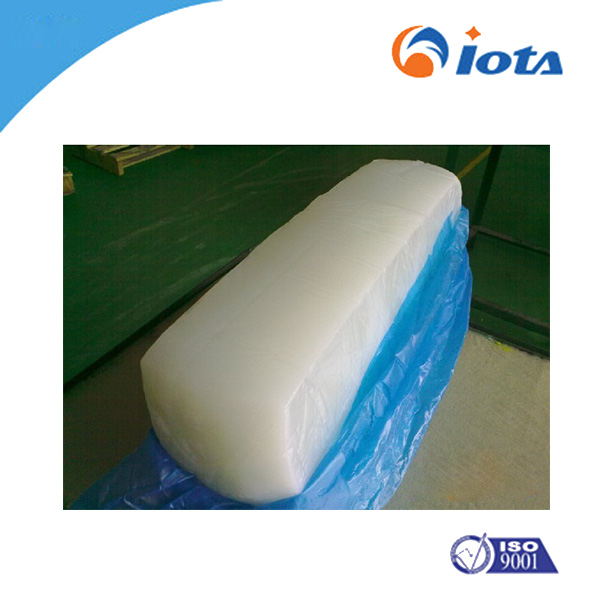
High damping coefficient and resistance to low temperature IOTA MM 771 Series
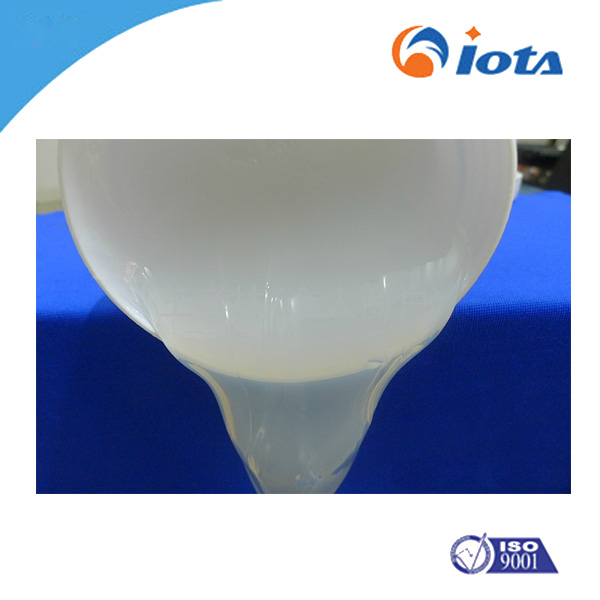
High temperature stability silicone rubber IOTA THT
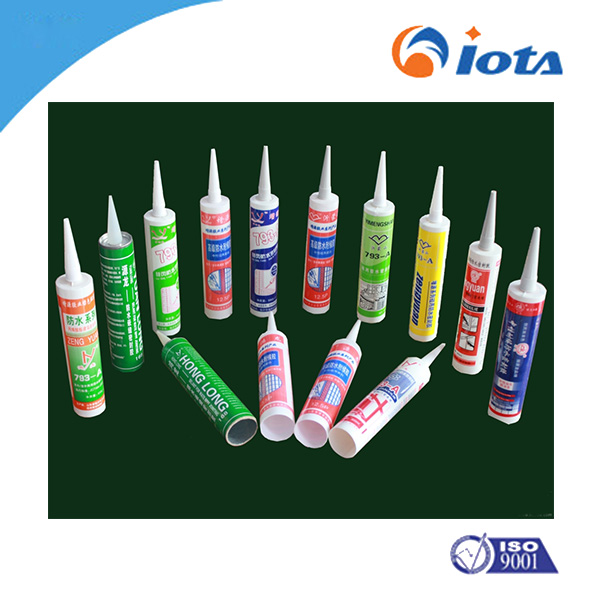
Outstanding high mechanical properties silicone rubber IOTA HP Series
High rebound and low compression set silicone rubber IOTA HCR 2900 Series
Good mechanical properties general silicone rubber IOTA HCR 1900 Series
Economic general silcone rubber IOTA HCR 1600 Series
Process ability silicone rubber IOTA HCR 9100 Series
High rebound silicone rubber IOTA HCR 900 Series
High tear stength and high transparent silicone rubber IOTA HCR 300 Series
High transparent extrusion silicone rubber IOTA HCR 100 Series
IOTA 795 Methyl vinyl silicone rubber
IOTA 759 Methyl vinyl silicone rubber
IOTA 755 Methyl vinyl silicone rubber
IOTA 753 Methyl vinyl silicone rubber
IOTA 751Methyl vinyl silicone rubber
IOTA107 V150000-V550000 High viscosity linear hydroxyl-terminated polydimethylsiloxane
IOTA107 V5000-V80000 low viscosity linear hydroxyl-terminated polydimethylsiloxane
IOTA 107 V500-V3000 low viscosity linear hydroxyl-terminated polydimethylsiloxane
IOTA1021Cyclopentasiloxane IOTA 1022Dimethiconol
Low compression set silicone rubber IOTA HCR 200 series
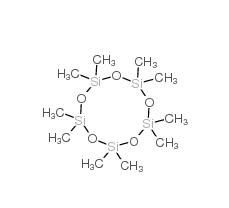
IOTA D5 Cyclopentasiloxane
RTV Methyl silicone rubber
Methyltrichlorosilane
Methyldichlorosilane
Dimethyl siloxane cyclics mixture
Dimethylchlorosilane
Silica
Octamethylcy-clotetrasiloxane
High efficient automobile detergent IOTA111
High efficient laundry detergent IOTA110
Smooth softener IOTA 17530
Polyester fluffy agent IOTA 17540
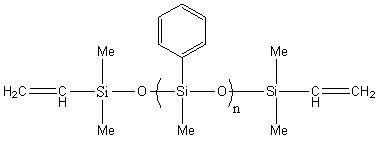
Divinyl-terminated methyl phenyl siloxane IOTA252
Methyl MQ silicone resin IOTA1200
Methyl MQ silicone resin IOTA7080 (powder)
Mica adhesive IOTA-500
Wetting agent IOTA245
High temperature mold release agent
High temperature resistant silicone oil
water soluble silicone oil IOTA-1291
Polydiethylsiloxane (lubricant oil or instrument oil )
Dicyclopentyldimethoxysilane (D-Donor)
Cyclohexyl methyl dimethoxysilane (CMMS)
Tetra methylethylketoxime silane TOS
Methyltris methylethylketoxime silane (MOS)
Tetrapropoxysilane IOTA-933
Mercaptopropyltrimethoxysilane IOTA-80
Methacryloylpropyltrimethoxysilane IOTA-70
Epoxypropoxypropyl trimethoxysilane IOTA-60
Methyl phenyldimethoxysilane MPDMS
Diphenyldimethoxysilane DDS
Aminoethyl aminopropyl trimethoxysilane DAMO
Aminopropyltriethoxysilane AMEO
Vinyltrismethylethylketoximesilane VOS
Tetravinyltetramethylcyclotetrasiloxane V4
Vinyltrimethoxysilane VTMO
High performance lubricant release agent
Glassine silicone paper
CCK Silicone Paper
CCK Release Paper
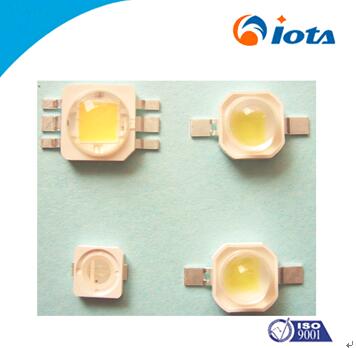
High refractive index LED package silicone gel IOTA4011
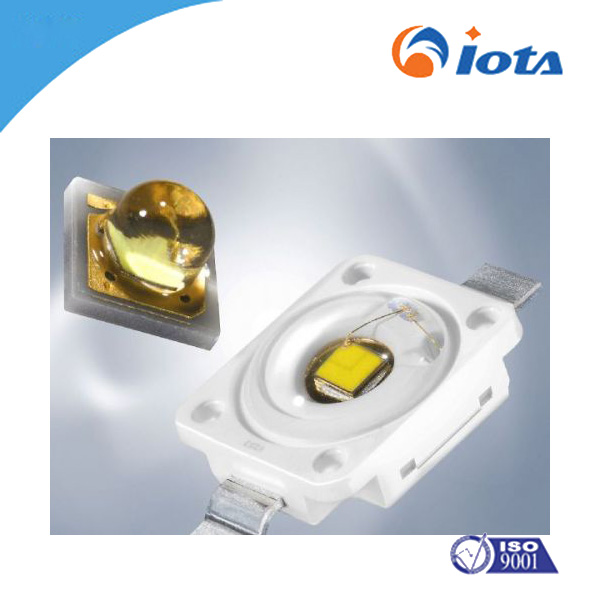
High refractive index LED package silicone gel IOTA4022
LED package Silicone gel IOTA3011
LED package silicone gel thickener IOTA204
Phenyl methyl hydrogen silicone resin IOTA-2207
Methyl phenyl vinyl silicone resin IOTA208
Phenyl-trisilane
Hexamethyldisilazane
Hexamethyldisiloxane IOTA 005
Triphenylchloromethane
7-methyl-3-siloxane
epoxy silicone oil
pigment printing thickener
polyester printing thickener
Chemical Fiber smoothing agent
Polyester smooth agent
Hydrogen termniated silicone oil
Tetramethyldisiloxane IOTA 606
Methyl Low Hydrogen silicone oil
Methyl High Hydrogen silicone oil
Dimethyl chlorosilane
TETRAMETHYLCYCLOTETRASILOXANE
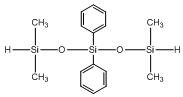
Tetramethyl diphenyl trisiloxane
Hydride terminated polyphenylsiloxane
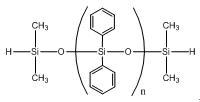
Hydride terminated polydiphenylsiloxane
Hydrogen MQ resin
Vinyl silicone oil
Side chain type vinyl silicone oil
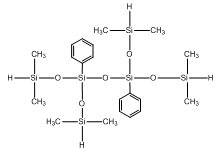
Tetramethyl diphenyl tetrasiloxane
Methyl silicone oil emulsion
Long chain alkyl silicone oil IOTA 2320
Divinyltetramethyldisiloxane(Vinyl double heads) IOTA 1002
Methyl phenyl resin IOTA-955
Methyl silicone resin IOTA 6070
Amino silicone oil IOTA 100
Amino silicone oil emulsions
Block amino silicone oils
Low viscosity silicone oils and Volatile silicone oils
Dimethicone methyl silicone oils IOTA 201
Hydroxyl silicone oils
Thread silicone oils IOTA205
High grade release papers
Glassine paper
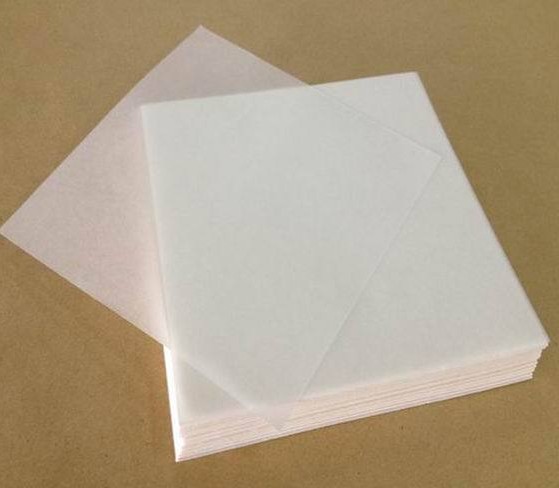
Food grade greaseproof papers
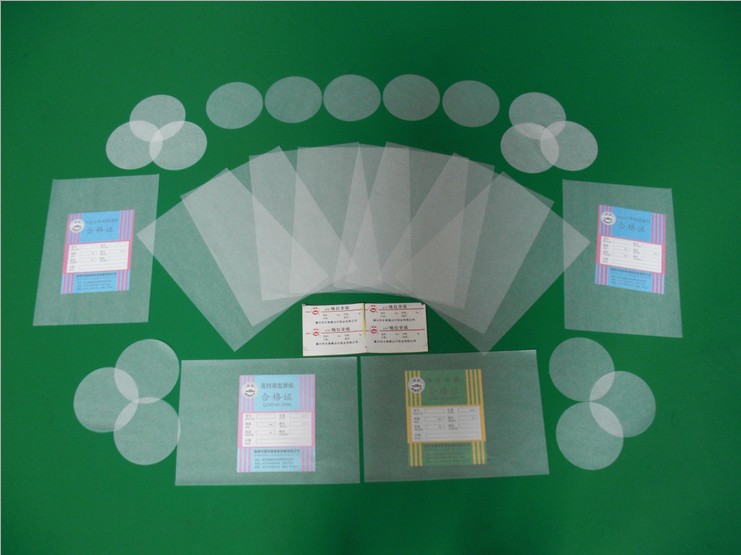
Food grade silicone papers
Leveling Agents Iota3000
Agricultural silicone surfactants IOTA-2000
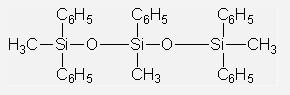
Vacuum Diffusion Pump Oils IOTA705
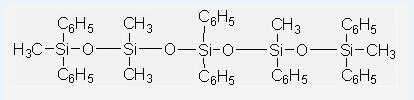
Phenyl Methyl Silicone Oils IOTA250-30
Phenyl Methyl Silicone Oils IOTA255
Phenyl Methyl silicone oil IOTA 556 (Phenyl Trimethicone, Cosmetic grade fluid)
Vacuum Diffusion Pump Oils IOTA702
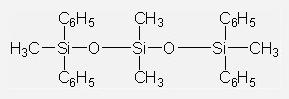
Vacuum Diffusion Pump Oils IOTA704
皖ICP备14007495号
Copyright © 2000-2026 Iota Silicone Oil (Anhui) Co., Ltd, All Rights Reserved


